This website uses cookies and similar technologies (“cookies”). Subject to your consent, will use analytical cookies to track which content interests you, and marketing cookies to display interest-based advertising. We use third-party providers for these measures, who may also use the data for their own purposes.
You give your consent by clicking "Accept all" or by applying your individual settings. Your data may then also be processed in third countries outside the EU, such as the US, which do not have a corresponding level of data protection and where, in particular, access by local authorities may not be effectively prevented. You can revoke your consent with immediate effect at any time. If you click on "Reject all", only strictly necessary cookies will be used.
A high pressure laminate and compact panel manufacturer established in 1998.
Views: 0 Author: Serena Sun Publish Time: 2026-09-22 Origin: Site
Why Does HPL Cabinet Edge Banding Turn Black?
Black lines along HPL cabinet edges can appear shortly after fabrication or develop after months of use. The discoloration may look like a defect in the decorative laminate, but its actual cause can involve the edge banding adhesive, exposed laminate core, substrate moisture, surface contamination, or inadequate bonding.
In cabinets made with 1mm high-pressure laminate (HPL), the decorative sheet is typically bonded to a substrate such as MDF or particleboard. The cut edges are then finished with HPL, ABS, PVC, or another compatible edge material. Because the surface laminate, substrate, adhesive, and edge band form an assembled system, problems in any component can affect the finished joint.
Key point: A dark cabinet edge does not automatically mean that the HPL sheet is defective or that moisture has caused mold. The appearance, location, and condition of the joint should be examined before identifying the cause or deciding whether repair is necessary.
This guide explains how high-pressure laminate sheets are bonded and edge-banded, why dark glue lines and black stains occur, and how cabinet manufacturers, fabricators, and project buyers can reduce the risk of recurring defects.
How to Identify Different Types of Black HPL Cabinet Edges
Before adjusting an edge banding machine or replacing a cabinet panel, determine whether the dark area is part of the original edge construction or a defect that developed later.
Visible Symptom
Possible Cause
Recommended Inspection
Uniform dark line visible from installation
Exposed HPL core, contrasting adhesive, or edge material
Compare the edge detail with an unused panel sample
Dark spots or particles inside the glue line
Contaminated or thermally degraded adhesive
Inspect the adhesive application system and glue residue
Black or gray marks that wipe off
Dust, grease, cleaning residue, or surface deposits
Perform a small-area cleaning test using an approved cleaner
Dark seam with edge lifting or substrate swelling
Moisture exposure, poor adhesion, or an open joint
Check edge separation, substrate condition, and moisture exposure
Intermittent black gaps along the edge
Inconsistent glue coverage, poor milling, or inadequate pressure
Examine a sample joint and verify machine settings
Discoloration concentrated around sinks or wet areas
Repeated water exposure or contamination
Check adjacent joints, sealant condition, and exposed substrate
These symptoms are diagnostic indicators rather than proof of a specific cause. Several problems can occur together, especially when the cabinet has experienced repeated cleaning, humidity, and temperature changes.
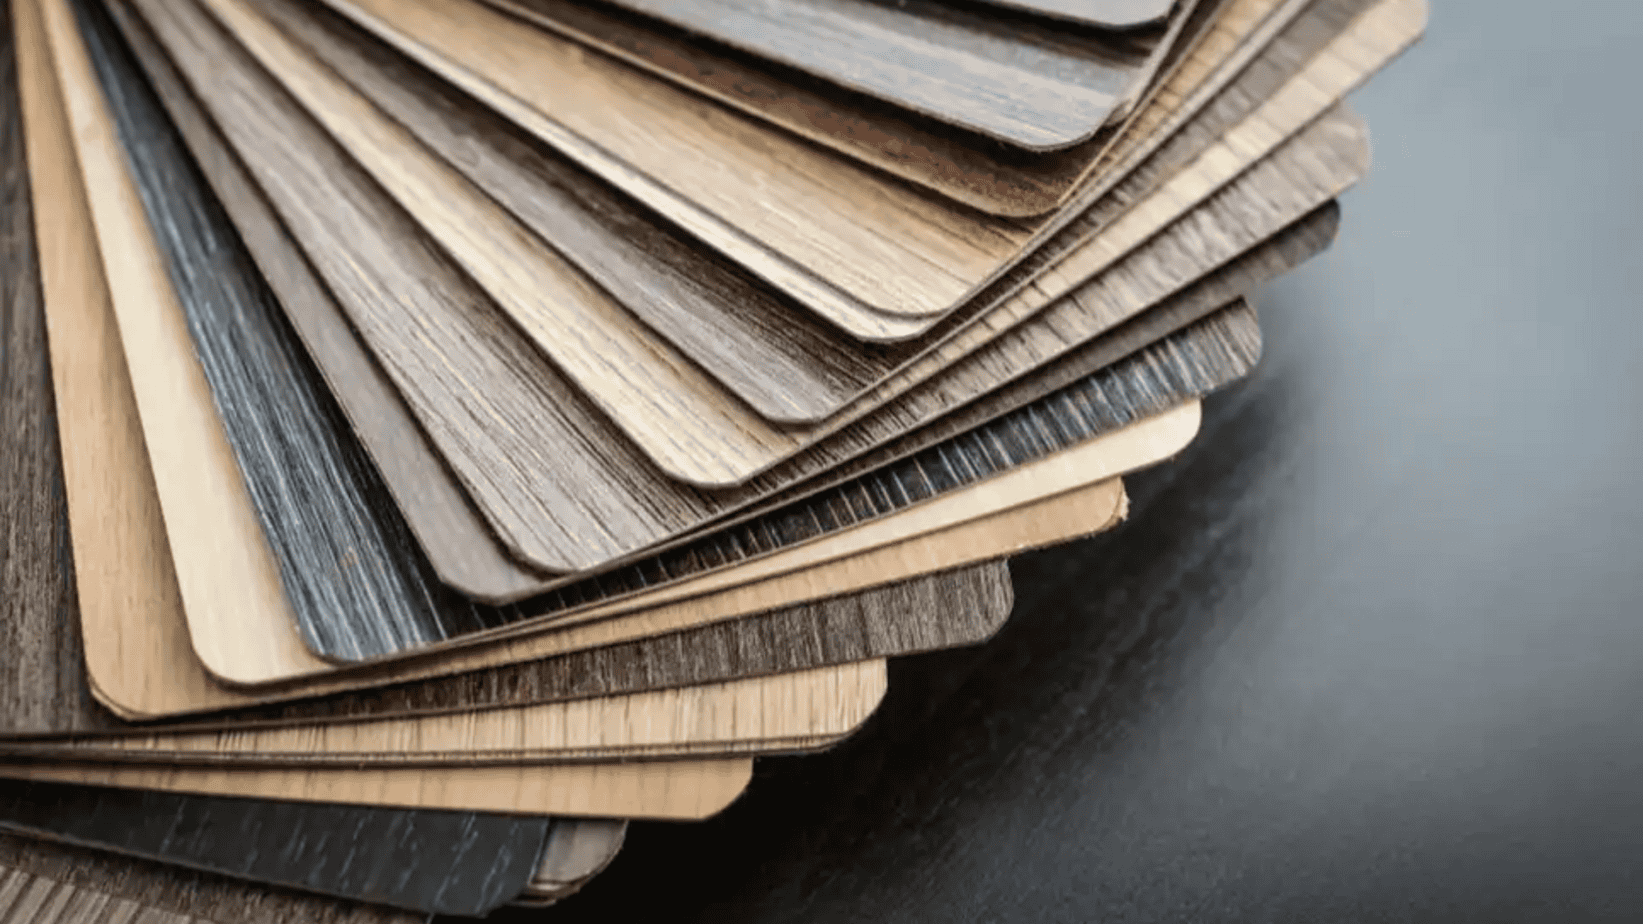
1mm HPL Lamination Process for Cabinet Panels
Thin decorative HPL and solid compact laminate are not interchangeable materials. Conventional 1mm HPL is generally used as a facing sheet bonded to a supporting panel, while compact HPL is a thicker, self-supporting laminate available for applications with different structural requirements.
For furniture and cabinet production, the performance of the finished assembly depends on substrate selection, adhesive compatibility, lamination conditions, balancing, and edge finishing.
HPL surface lamination and cabinet panel fabrication require compatible materials and controlled processing conditions.
Step 1: Prepare the MDF or Particleboard Substrate
Before applying decorative HPL, the substrate should be flat, stable, clean, and suitable for the intended application. MDF and particleboard are common furniture substrates, but their surface quality, density, and moisture condition can influence bonding performance.
Remove machining dust, grease, loose particles, and other contamination. Inspect the panel for surface irregularities, damage, and excessive moisture. Defective substrate preparation may produce uneven adhesive contact, localized bonding failures, or visible imperfections in the finished laminate.
Step 2: Select a Compatible HPL Lamination Adhesive
The adhesive used to bond a decorative HPL sheet to the panel face is not necessarily the same adhesive used for edge banding. Depending on the production process, suitable HPL lamination systems may use contact adhesives, PVA-based adhesives, or other approved bonding technologies.
Adhesive selection should consider the laminate backing, substrate type, production equipment, press method, and anticipated service conditions. Follow the adhesive manufacturer's instructions for application quantity, assembly time, temperature, pressure, and curing.
Applying too little adhesive can leave poorly bonded areas. Excessive or uneven application may contribute to surface irregularities or adhesive residue.
Step 3: Control the Pressing and Bonding Process
HPL cabinet panels may be manufactured using hot-press, cold-press, or other bonding processes, depending on the adhesive system and equipment.
For a hot-press process, the fabricator should control the prescribed temperature, pressure, and pressing time. Other adhesive systems may require different assembly and curing conditions. There is no single universal temperature or pressure setting suitable for all 1mm HPL lamination systems.
After bonding, inspect the panel for flatness, bubbles, lifting, and inconsistent adhesion before proceeding to cutting and edge finishing.
Step 4: Allow Proper Conditioning and Consider Panel Balancing
Laminated panels should be handled and processed in accordance with the adhesive's curing and conditioning requirements. Cutting or machining before adequate bond development may affect the finished assembly.
For panel constructions where warping is a concern, an appropriate balancing laminate or backing sheet may be required on the opposite face. The correct construction depends on panel dimensions, substrate, and application.
Professional Edge Banding Process for HPL Cabinet Panels
After the decorative laminate has been bonded to the substrate, the exposed panel edges are finished using a compatible edge material. The goal is to achieve a secure bond, consistent appearance, and joint construction appropriate for the service environment.
Step 1: Precision Cutting and Edge Pre-Milling
The panel edge must provide a suitable bonding surface. Saw marks, chipped laminate, loose particles, and an out-of-square edge can prevent uniform adhesive contact.
Where applicable, a pre-milling operation removes machining irregularities and prepares a flat, consistent edge before adhesive application.
Step 2: Match the Edge Banding Material
Common options for decorative HPL cabinet panels include ABS edge banding, PVC edge banding, and HPL laminate edging.
The edge material should be selected according to panel thickness, decorative finish, edge profile, processing equipment, and expected conditions of use. Matching the surface color alone is not sufficient; gloss, texture, thickness, and the appearance of the glue line also influence the finished result.
Step 3: Control Hot-Melt Adhesive Application
EVA and reactive PUR are commonly used hot-melt adhesive technologies in industrial edge banding. Each has its own operating characteristics and processing requirements.
Adhesive temperature, application quantity, feed speed, open time, and material conditioning must be compatible. Excessive heating or prolonged exposure to heat can degrade some adhesives, while insufficient operating temperature can lead to poor wetting and weak bonding.
The correct settings must come from the selected adhesive's technical data sheet and the equipment manufacturer's instructions.
Step 4: Apply Consistent Pressure and Complete Edge Finishing
Pressure rollers should provide consistent contact between the edge band, adhesive, and prepared substrate. Insufficient contact pressure, incorrect alignment, or uneven adhesive distribution can produce weak joints and visible gaps.
After bonding, the edge is trimmed, scraped, and polished as appropriate. Inspect the finished joint for excessive glue squeeze-out, exposed gaps, sharp edges, and surface damage.
HPL cabinet surfaces and finished edges should be evaluated together for appearance, bonding quality, and suitability for the intended environment.
Main Causes of HPL Cabinet Edge Blackening
1. Moisture Penetration Through Open Edge Joints
Moisture entering an inadequately bonded edge joint can damage a wood-based substrate. MDF and particleboard are particularly vulnerable when exposed to sustained or repeated moisture beyond their intended conditions of use.
Kitchen cabinets near sinks, dishwashers, and cleaning areas may experience repeated exposure to water and steam. If moisture reaches the substrate, swelling, deterioration, joint opening, or discoloration may develop.
Dark staining can also be associated with microbial growth under suitable conditions, but the presence of mold cannot be established from a black line alone. Moisture damage should be investigated rather than assumed.
2. Contaminated or Overheated Edge Banding Adhesive
Hot-melt adhesive can deteriorate when processed outside its recommended temperature range or exposed to excessive heat for prolonged periods. A poorly maintained glue application system may also introduce degraded adhesive particles into fresh material.
Discolored adhesive may leave dark specks or an unattractive line between the edge band and decorative panel surface. This can be particularly visible on white or light-colored HPL cabinets.
Check the glue pot or melting system, temperature control, application roller or nozzle, and cleaning procedure. Replacing adhesive without investigating the equipment may not correct the underlying problem.
3. Poor Edge Milling and Incomplete Adhesive Coverage
An uneven substrate edge may prevent full contact between the edge band and the panel. Milling grooves, damaged corners, dust, or insufficient adhesive coverage can create localized voids.
These gaps may appear as dark intermittent lines and can collect dirt during use. Where the bond is weak, edge lifting or peeling may also occur.
Improving the pre-milling operation, verifying adhesive coverage, and checking pressure roller alignment can help address these problems.
4. Surface Contamination and Improper Cleaning
Kitchen grease, dust, polishing residue, and unsuitable cleaning agents can accumulate along the joint between the HPL surface and edge band.
Some apparent blackening problems are surface contamination rather than adhesive or substrate failure. Before dismantling an otherwise sound panel, inspect the joint and test a cleaning method approved for both the decorative laminate and the edge material.
Avoid abrasive cleaning methods or aggressive solvents unless specifically permitted by the relevant material manufacturer.
5. Material Movement and Incompatible Bonding Conditions
HPL, wood-based substrates, and thermoplastic edge materials respond differently to changes in temperature and humidity.
If materials are poorly conditioned, inadequately bonded, or used outside their intended environmental conditions, movement may place stress on the joint and contribute to gap formation or edge lifting.
Conditioning materials before fabrication, selecting compatible adhesives, and following installation requirements help reduce these risks.
6. Exposed Dark HPL Core at the Edge
Not every dark line is a manufacturing failure. Conventional HPL often contains a kraft-paper-based core that can appear darker than the decorative surface.
In certain self-edge constructions or exposed laminate joints, this contrast creates a visible brown or dark line even when the assembly is otherwise properly manufactured.
For projects requiring a more uniform edge appearance, fabricators can evaluate suitable decorative edging profiles, color-matched edge materials, or alternative laminate constructions. The final appearance should be confirmed using an approved sample.
EVA vs PUR Adhesive for HPL Cabinet Edge Banding
Adhesive selection is an important part of cabinet edge design. EVA hot-melt and reactive PUR hot-melt systems are both used in furniture production, but their behavior and equipment requirements differ.
Comparison
EVA Hot-Melt Adhesive
Reactive PUR Hot-Melt Adhesive
Bonding mechanism
Thermoplastic bonding through heating and cooling
Initial physical setting followed by moisture-triggered chemical curing
Moisture resistance
Depends on the selected grade and joint design
Suitable grades can provide higher moisture resistance after curing
Heat resistance
Depends on formulation and operating conditions
Suitable grades can offer improved heat resistance
Processing requirements
Compatible melting and application equipment
Suitable moisture-sensitive adhesive handling and application equipment
Typical consideration
General interior furniture production
Applications requiring enhanced joint resistance to moisture or heat
Important: PUR adhesive is not a substitute for a properly prepared substrate, suitable edge material, or accurate machine settings. Even a high-performance adhesive cannot reliably compensate for an open or poorly formed joint.
Processing temperatures and curing conditions vary by adhesive formulation. Consult the adhesive supplier's technical documentation rather than applying a universal machine temperature to all EVA or PUR products.
How to Troubleshoot Black HPL Edge Banding
A systematic inspection can help cabinet manufacturers distinguish cosmetic discoloration from a bonding or substrate problem.
Step 1: Record When and Where the Black Line Appeared
Determine whether the line was visible immediately after production or developed during use. Record the cabinet location, surrounding humidity, cleaning practices, and affected panel edges.
A dark line present from the beginning may indicate the laminate core or adhesive color. Progressive discoloration accompanied by swelling or peeling requires further investigation.
Step 2: Inspect the Physical Condition of the Joint
Check whether the edge band remains firmly attached, whether a visible gap has opened, and whether the substrate has swollen or softened. A narrow cosmetic line and a loose edge band require different corrective actions.
Step 3: Check for Removable Surface Contamination
On an inconspicuous area, use a cleaner approved for the HPL surface and edge material. If the discoloration is removed without affecting the joint, surface deposits may have contributed to the problem.
Step 4: Examine a Representative Sample Joint
Where practical, a qualified fabricator can inspect a removed sample or production offcut to examine the adhesive layer, edge coverage, and substrate condition. Cross-sectional inspection can help reveal voids, uneven glue application, or moisture-related damage.
Step 5: Review Production and Material Records
Compare the affected cabinet with production records, retained samples, and other panels from the same batch. Review adhesive type, machine settings, substrate condition, edge material, and maintenance records where available.
If similar defects appear across multiple production batches, investigate the process and material combination before restarting large-volume production.
How to Prevent HPL Cabinet Edge Banding Defects
Preventive quality control should cover the entire laminated panel construction, not only the visible edge joint.
Production Stage
Quality Control Item
Purpose
Material selection
Confirm HPL, substrate, edge band, and adhesive compatibility
Reduce material mismatch
Storage and conditioning
Control moisture exposure and follow material conditioning instructions
Limit dimensional instability
HPL lamination
Check substrate cleanliness, adhesive coverage, pressing, and bond quality
Reduce lamination defects
Cutting and pre-milling
Inspect cutting accuracy, edge flatness, and loose particles
Prepare a consistent bonding surface
Adhesive application
Verify adhesive condition, operating temperature, and coverage
Reduce contamination and poor bonding
Edge bonding
Check roller pressure, alignment, and feed conditions
Improve joint consistency
Final inspection
Examine glue lines, trimming, edge lifting, and finished appearance
Identify defects before delivery
Packing and transport
Protect panels against water exposure and edge impact
Reduce handling and storage damage
For repeat production, an approved reference sample can help define acceptable edge color, joint visibility, adhesive appearance, and workmanship. Inspection criteria should be agreed upon before manufacturing begins.
Can Black HPL Cabinet Edges Be Repaired?
The appropriate repair depends on whether the problem is cosmetic, adhesive-related, or structural.
Surface Staining Without Joint Damage
If the edge remains secure and the dark marks consist of removable dirt or grease, careful cleaning may restore the appearance. Use cleaning products approved by the laminate and edge material manufacturers.
Visible Glue Line or Minor Edge Banding Failure
Some localized edge banding defects may be repairable by a qualified fabricator. Depending on the panel condition, replacing the affected edge band or correcting the bonding process may be possible.
However, cosmetic treatments cannot reliably restore a joint with inadequate adhesion, and covering an open seam without addressing its cause may allow the problem to recur.
Swollen MDF or Particleboard Substrate
If moisture has caused significant swelling, loss of integrity, or persistent deterioration of the substrate, cleaning or re-banding alone may be insufficient. Depending on the extent of damage, partial component replacement or complete panel replacement may be required.
The moisture source should also be identified and corrected before new components are installed.
Selecting 1mm HPL Sheets for Cabinet Manufacturing
For cabinet manufacturers, furniture brands, distributors, and commercial project contractors, selecting the correct decorative laminate is the starting point for a reliable finished panel.
POLYBETT supplies decorative HPL products for furniture and interior applications. When evaluating matte-finish HPL sheets for furniture or high-gloss decorative HPL sheets, buyers should review the complete panel construction rather than judging the decorative surface alone.
Important information to confirm before ordering includes:
Required HPL sheet thickness, including whether 1mm laminate is appropriate
Decorative color, surface texture, and gloss requirements
Panel dimensions and intended substrate material
Face lamination adhesive and production method
Matching ABS, PVC, or HPL edge banding material
Expected indoor environment and exposure to moisture or heat
Approved finished-edge appearance and quality criteria
Applicable product documentation and project specifications
Providing this information helps suppliers and fabricators evaluate material suitability and identify potential compatibility issues before production.
Frequently Asked Questions About HPL Cabinet Edge Blackening
Why does HPL cabinet edge banding turn black after one year?
Blackening after several months may result from dirt accumulation, adhesive discoloration, moisture entering a defective joint, or deterioration of the substrate. A dark line may also have existed from installation because of the laminate core or edge construction. The cause should be determined through inspection rather than the age of the cabinet alone.
Does black edge banding mean that mold is growing inside the cabinet?
No. Black or dark edge discoloration can have several causes, including adhesive contamination, exposed HPL core, surface staining, and moisture damage. Mold is possible in damp conditions, but color alone does not confirm microbial growth.
Is 1mm HPL suitable for kitchen cabinets and furniture panels?
Yes. A suitable 1mm decorative HPL sheet can be used as a facing material for properly designed furniture and cabinet panels. Performance depends on the laminate grade, substrate, adhesive system, edge construction, and installation conditions. The finished assembly should be evaluated for the intended application.
What is the difference between 1mm HPL and compact laminate?
Conventional 1mm decorative HPL generally requires bonding to a supporting substrate, whereas compact laminate is a thicker, self-supporting panel used in suitable structural and decorative applications. Their edge construction, machining requirements, and material appearance differ, so they should not be treated as direct substitutes without reviewing the project specifications.
Is PUR edge banding adhesive better than EVA for kitchen cabinets?
Reactive PUR adhesives can offer enhanced moisture and heat resistance compared with many conventional EVA formulations. However, the final result depends on the specific adhesive grade, substrate, edge material, processing equipment, and joint quality. Both systems require correct application conditions.
How can manufacturers prevent dark glue lines on white HPL cabinets?
Manufacturers should select a compatible adhesive with an appropriate color, maintain clean application equipment, control processing conditions, prepare the substrate edge accurately, and inspect adhesive coverage. An approved edge sample helps establish acceptable visual quality before mass production.
Can black stains along HPL cabinet edges be cleaned?
Surface dirt and some deposits may be removable using approved cleaning methods. However, cleaning cannot eliminate an exposed dark laminate core, restore a failed adhesive joint, or reverse significant substrate swelling. Identify the source of discoloration before attempting repair.
Which is better for HPL cabinet edging: ABS, PVC, or HPL?
Each material has different processing and appearance characteristics. ABS and PVC are common thermoplastic edging options, while HPL edging can provide a coordinated laminate finish. The choice depends on edge geometry, desired appearance, adhesive compatibility, machine capability, and the project's performance requirements.
What should buyers check before accepting finished HPL cabinet panels?
Buyers should examine surface flatness, laminate adhesion, edge band alignment, visible glue lines, edge lifting, trimming quality, and signs of substrate damage. For commercial procurement, these checks should be compared with approved samples and agreed acceptance criteria.
Technical References for HPL Lamination and Edge Banding
The following manufacturer resources provide additional information on decorative laminate construction, edge banding materials, adhesives, and fabrication requirements:
Material and adhesive recommendations should always be checked against the latest applicable product documentation and actual fabrication conditions.
Conclusion: Preventing Black Edges in HPL Cabinet Manufacturing
HPL cabinet edge blackening should be treated as a problem that requires accurate diagnosis rather than an automatic indication of defective laminate. Dark lines can result from visible core material, adhesive discoloration, contamination, poor edge bonding, or moisture-related deterioration.
For furniture manufacturers and commercial cabinet projects, a reliable result starts with selecting suitable 1mm HPL sheets, compatible substrates and adhesives, accurately machined edges, and consistent production controls. Inspection of both appearance and bond integrity is essential.
If you are sourcing decorative HPL for cabinet doors, furniture panels, shelving, or commercial interiors, contact POLYBETT to discuss available laminate products and your project specifications.
The general manager of Changzhou Zhongtian Fire-resistant Decorative Board Co., Ltd., has been deeply involved in the HPL fireproof board industry for 15 years.
 Русский
 English
 العربية
 Français
 Español
 Português
 Deutsch
 italiano
 日本語
 한국어
 Nederlands
 Tiếng Việt
 ไทย
 Polski
 Türkçe
 አማርኛ
 Bahasa Melayu
 தமிழ்
 Filipino
 Bahasa Indonesia
 magyar
 Română
 Монгол
 қазақ
 Српски
 हिन्दी
 فارسی
 Kiswahili
 Slovenčina
 Slovenščina
 Svenska
 українська
 Ελληνικά
 Suomi
 Հայերեն
 עברית
 اردو
 Shqip
 বাংলা
 Hrvatski
 Afrikaans
 Māori
 සිංහල
 Oʻzbekcha
 latviešu
 Беларуская мова
 Bosanski
 Български
 ქართული
 Lietuvių
 Malti
 Runasimi